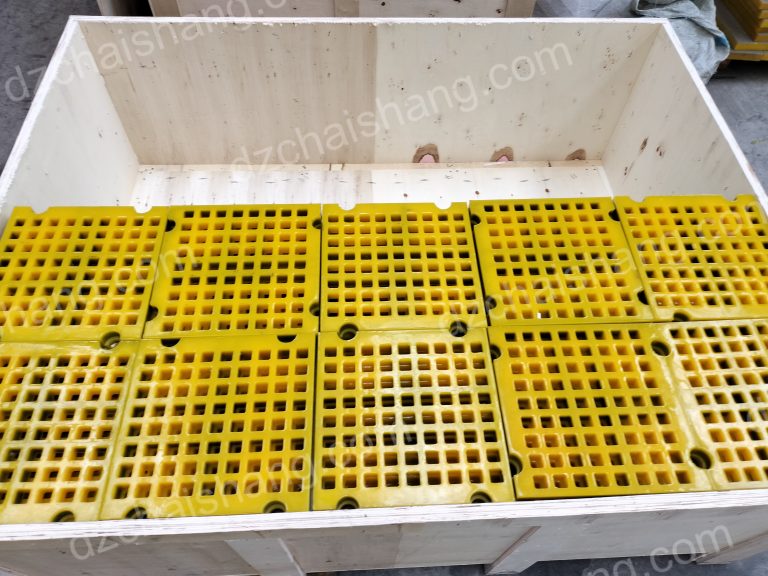

What Affects Wear Life of Rubber Screen Mesh?
What Affects Wear Life of Rubber Screen Mesh?
If you're troubleshooting premature failure or comparing suppliers, understanding what affects the wear life of rubber screen mesh is the first step toward smarter procurement. The frustrating reality? Most buyers focus on a single variable — material type or price — and miss the interplay of factors that actually determines how long a screen lasts. The solution is a systems-level approach to specification and selection.
Rubber screen mesh wear life is not determined by any single factor. It is the combined outcome of rubber compound formulation, screen structural design (aperture geometry, open area ratio, rib thickness), and actual operating conditions including feed material properties, vibration parameters, moisture content, and maintenance practices. Buyers who match all three variables to their specific application consistently achieve the longest service life — regardless of brand or price point.

A common question we receive from mining and aggregate buyers is simply: "Which rubber screen mesh lasts the longest?" But before we can answer, we need to know at least a dozen things about the operation. Below, I'll walk you through each factor that shapes wear life — and more importantly, how to use these factors as a decision framework when specifying your next screen.
Does Rubber Compound Formulation Determine Screen Mesh Wear Life?
Material selection is the first lever most buyers reach for when evaluating rubber screen mesh. It seems intuitive: pick the most abrasion-resistant compound, and the screen lasts longer. But in our experience helping clients match screen specifications to their operations, compound performance is always conditional.
The right rubber compound depends on the specific demands of your application — ore hardness, particle shape, moisture, chemical exposure, and operating temperature. No single compound wins in all conditions. Natural rubber (NR), styrene-butadiene rubber (SBR), and polyurethane (PU) each have distinct advantages that emerge or disappear depending on the environment.

How Do NR, SBR, and PU Compare Under Different Conditions?
Let me break down what we typically observe in practice across different screening environments:
| Property | Natural Rubber (NR) | SBR | Polyurethane (PU) |
|---|---|---|---|
| Dry abrasion resistance | Good | Good–Very Good | Excellent |
| Wet abrasion resistance | Very Good | Moderate | Reduced (hydrolysis risk) |
| Tear resistance | Excellent | Good | Moderate–Good |
| Chemical/oil resistance | Poor | Moderate | Good–Excellent |
| Low-temperature flexibility | Good | Moderate | Poor–Moderate |
| Cut/gouge resistance (coarse, angular feed) | Very Good | Good | Moderate |
| Typical hardness range (Shore A) | 40–70 | 50–75 | 60–95 |
Key insight: PU is often marketed as the "most wear-resistant" option, and in dry, fine-particle screening of moderate-hardness materials, that's generally true. But introduce high moisture, large angular particles, or sub-zero temperatures, and PU's advantage can vanish — or even reverse. I've seen clients switch from PU to NR in wet iron ore screening and gain 30–40% more service life, simply because the conditions favored NR's superior tear and wet abrasion characteristics.
Why Compounding Quality Matters as Much as Polymer Type
Beyond the base polymer, the quality of compounding — filler types, plasticizer ratios, vulcanization parameters, and antioxidant packages — has a dramatic impact on wear life. Two screens both labeled "natural rubber" can differ in actual abrasion resistance by 40% or more depending on the formulation and processing quality.
In our experience, key quality indicators buyers should verify include:
- Tensile strength and elongation at break — documented on material test certificates
- Abrasion loss (DIN or Akron method) — lower is better, but always ask under what test conditions
- Hardness consistency — variation across a single panel suggests poor vulcanization control
- Whether recycled or reclaimed rubber is blended in — this is common in low-cost screens and significantly reduces fatigue life
A buyer who specifies "NR, 55 Shore A" without asking for compound test data is essentially buying blind. I always recommend requesting material certificates and, where possible, comparing them against a known benchmark from a previous order that performed well.
How Does Screen Structure and Aperture Design Affect Wear Life?
Even with the perfect rubber compound, a poorly designed screen structure will fail prematurely. Screen geometry — aperture shape, open area percentage, rib cross-section, and overall panel thickness — directly controls how stress and abrasive material interact with the screen surface. This is where many procurement decisions go wrong.
The structural design of rubber screen mesh governs both throughput efficiency and mechanical durability. Higher open area increases capacity but reduces the rubber material available to resist wear and impact. Every structural specification is a trade-off between screening performance and wear life. Buyers who demand maximum open area without understanding this trade-off consistently experience premature failure.

Open Area: The Trade-Off Most Buyers Miss
Open area is the percentage of the screen surface occupied by apertures rather than solid rubber. It's the primary driver of throughput capacity, so buyers naturally want it as high as possible. But here's what happens as open area increases:
- Rib width decreases — less rubber between apertures means faster localized wear-through
- Structural rigidity decreases — the panel deflects more under load, concentrating stress at connection points
- Tear propagation risk increases — once a crack initiates at a thin rib, it spreads faster through less material
In practice, we typically see the following relationship:
| Open Area Range | Typical Application | Wear Life Implication |
|---|---|---|
| 25–35% | Heavy-duty primary scalping, high-impact zones | Longest wear life, lowest throughput |
| 35–50% | General classification, mid-range aggregate | Balanced durability and capacity |
| 50–65%+ | Fine screening, dewatering, high-capacity demand | Shortest wear life, highest throughput |
The screen didn't fail — the specification was wrong. This is a phrase I find myself using regularly. When a client reports that a screen "only lasted 3 weeks," the first question isn't about material quality — it's about whether the open area and rib dimensions were appropriate for the feed conditions. In roughly half of premature failure cases we investigate, the root cause traces back to an over-aggressive open area specification, not a material defect.
Aperture Shape and Rib Profile
Square, rectangular, slotted, and hexagonal apertures each create different wear patterns. Rectangular and slotted apertures oriented along the material flow direction tend to wear more evenly but may blind faster with near-size particles. Square apertures offer versatile classification but can develop "hourglass" wear profiles at high-abrasion zones.
The rib profile — flat-top, tapered, or domed — also matters. A tapered rib sheds material more effectively and reduces blinding, but wears through the narrow section faster. A flat-top rib provides a larger initial wear surface but may retain fines and accelerate pegging.
The critical takeaway for buyers: always discuss aperture geometry and rib profile with your supplier in the context of your specific material and deck position. A screen that performs well on a top deck handling 50mm+ coarse aggregate will behave very differently on a bottom deck classifying 3–6mm material.
Why Are Operating Conditions the Largest Variable in Rubber Screen Mesh Wear Life?
You can specify the perfect compound and the ideal screen geometry, and still get poor wear life if operating conditions are working against you. In our experience, operating conditions account for the widest variance in rubber screen mesh lifespan between installations. Two identical screens on two different vibrating decks can have dramatically different service lives.
Operating conditions — including feed characteristics, vibration parameters, installation quality, and maintenance routines — create the actual wear environment that the screen must survive. These are external to the product itself, but they are the single largest determinant of real-world wear life. Buyers who treat wear life as a product attribute rather than a system outcome will always be disappointed.

Feed Material Properties
The material being screened is the most direct wear agent. Key feed properties include:
- Hardness (Mohs scale): Screening silica sand (Mohs 7) is fundamentally different from screening coal (Mohs 2–3). Higher ore hardness accelerates abrasive wear exponentially, not linearly.
- Particle size distribution: Oversized particles impact and gouge; near-size particles peg apertures and create localized stress concentrations. A well-graded feed wears screens more evenly than a poorly graded one.
- Particle shape: Angular, freshly crushed material cuts and tears rubber faster than rounded, naturally worn particles. This is especially critical when comparing PU (moderate cut resistance) vs. NR (superior tear resistance).
- Moisture content: Wet screening changes the abrasion mechanism. Water acts as a lubricant in some cases (reducing sliding friction) but can also cause hydroplaning, clay buildup, and — in the case of polyurethane — hydrolytic degradation over extended exposure.
- Chemical corrosiveness: Acidic or alkaline slurries attack certain rubber compounds. NR degrades in oily or chemically aggressive environments; PU handles many chemicals well but is vulnerable to prolonged high-temperature moisture.
Vibration Parameters and Machine Setup
The vibrating screen itself is part of the wear equation:
- Amplitude and frequency: Higher amplitude increases material throw and reduces blinding but also increases impact stress on the screen. Higher frequency with lower amplitude favors finer classification but can generate heat in the rubber through cyclic flexing.
- Stroke type: Circular, linear, and elliptical strokes each create different material flow and contact patterns across the screen surface.
- Deck inclination: Steeper angles move material faster (less contact time, less wear per unit area) but reduce screening efficiency. Flatter decks increase residence time and wear exposure.
- Screen tension: Rubber screen panels that are improperly tensioned — too loose or too tight — develop uneven deflection patterns. Loose panels flap and fatigue at mounting points; over-tensioned panels can't absorb impact energy and crack.
Feed Method and Distribution
How material hits the screen matters more than most buyers realize:
- Center feed vs. end feed: Center feeding concentrates impact and wear on the center of the panel. End feeding creates a more gradual distribution but can overload the feed end.
- Feed height and velocity: Material dropping from a significant height impacts the screen with more force, accelerating impact wear. Feed chutes, rock boxes, or curtains that slow material before it contacts the screen can extend wear life by 20–50% in high-impact applications — a low-cost modification with outsized returns.
- Feed rate consistency: Surging or slug feeding creates intermittent high-impact events that fatigue rubber faster than a steady feed at the same average tonnage.
Practical example: One of our clients in the aggregate sector was replacing rubber screen mesh every 6 weeks on a secondary classification deck. After reviewing their setup, we identified two issues: the feed chute was directing material at high velocity onto the first 300mm of the screen, and the panels were slightly under-tensioned. Installing a deflector plate and re-tensioning the panels — without changing the screen specification at all — extended wear life to approximately 14 weeks. The screens were never the problem.
Is Price a Reliable Indicator of Rubber Screen Mesh Quality?
When purchasing rubber screen mesh, it's tempting to use price as a shortcut for quality. Expensive must mean better; cheap must mean inferior. In our 30+ years of manufacturing and supplying screen mesh globally, I can tell you confidently that this shortcut fails in both directions. Price is a poor proxy for quality.
Low-priced rubber screen mesh may use recycled rubber, inferior fillers, or under-cured compounds that fail prematurely. But high-priced screens can also be over-specified for the application — paying for polyurethane performance in a low-abrasion application where natural rubber would last just as long at half the cost. The right purchasing framework is match-based, not price-based.

What to Look for Beyond Price
Instead of using price as your primary filter, I recommend evaluating suppliers and products on the following criteria:
- Material test certificates: Request documented tensile strength, elongation, hardness, and abrasion loss data. Reputable manufacturers using imported or controlled raw materials will provide these readily.
- Compounding transparency: Ask what base polymer is used, whether any recycled content is blended, and what the vulcanization process is. Suppliers who can't or won't answer these questions are a red flag.
- Dimensional consistency: Measure aperture sizes, rib widths, and panel thickness across multiple samples from the same order. Inconsistency suggests poor mold maintenance or process control.
- Application-specific recommendations: A supplier who asks detailed questions about your feed material, deck configuration, and performance expectations before quoting is more likely to deliver a screen that lasts than one who simply offers the cheapest or most expensive option.
- Track record and reference checks: Where possible, ask for references from similar applications. A screen that performed well in a gold processing plant may not be suitable for a limestone quarry — context matters.
The Real Cost Metric: Cost Per Tonne Screened
The only meaningful comparison between rubber screen mesh options is cost per tonne of material processed (or cost per operating hour, if tonnage data isn't available). This metric accounts for:
- Purchase price
- Installation labor and downtime cost
- Actual wear life in your specific application
- Screening efficiency (a cheap screen that blinds frequently and reduces throughput costs more per tonne than a more expensive screen that maintains efficiency)
| Metric | Cheap Screen | Mid-Range Screen | Premium Screen |
|---|---|---|---|
| Unit price | $X | $1.5X | $2.5X |
| Typical wear life (same application) | 4 weeks | 10 weeks | 12 weeks |
| Downtime per change (hrs) | 2 | 2 | 2 |
| Cost per operating week | Highest | Lowest | Moderate |
In this illustrative example, the mid-range screen — properly specified for the application — delivers the lowest total cost of ownership. The premium screen lasts slightly longer but not enough to justify the price differential. The cheap screen is the most expensive option once downtime is factored in.
How Should Buyers Specify Rubber Screen Mesh for Maximum Wear Life?
Bringing all these factors together, the real question isn't "what affects wear life" — it's "how do I specify the right screen for my application?" This is the reframe that separates buyers who consistently get good screen life from those who are perpetually troubleshooting.
To maximize rubber screen mesh wear life, buyers should follow an application-first specification process: define your feed material and operating conditions first, then select the compound and structural design that matches those conditions, and finally choose a supplier based on quality evidence and application support — not price alone.

A Practical Specification Framework
Here is the process I walk clients through when they're selecting or troubleshooting rubber screen mesh:
Step 1: Define the application environment
- What material is being screened? (Type, hardness, moisture, particle size range)
- What is the deck position? (Top/scalping, middle/classification, bottom/dewatering)
- What is the feed rate and method?
- What are the vibration parameters? (Amplitude, frequency, stroke type)
- What is the operating temperature range?
Step 2: Select the appropriate rubber compound
- Match compound properties to the dominant wear mechanism (abrasion, impact, tear, chemical attack)
- Consider environmental factors (moisture, temperature, chemical exposure)
- Request material test data from the supplier
Step 3: Specify screen structure and geometry
- Define the target cut size and acceptable open area range
- Balance throughput requirements against wear life expectations
- Discuss rib profile and panel thickness with the supplier
Step 4: Evaluate suppliers on quality evidence
- Material certificates, production consistency, compounding transparency
- Application engineering support — do they ask the right questions?
- References from comparable applications
Step 5: Monitor and optimize in service
- Track actual wear life against predictions
- Document wear patterns — uniform wear is good; localized wear indicates a design or operating issue
- Feed data back to your supplier for continuous improvement
The best client-supplier relationships I've been part of are iterative. The first